Weld defects are rarely caused by a single factor. In industrial metal fabrication, problems can come from inconsistent joint positioning, unsuitable welding parameters, excessive heat input, poor material preparation, fixture movement, or insufficient inspection. When these issues occur repeatedly in a production batch, the result can be more than an individual defective weld. Additional grinding, straightening, repair welding, dimensional adjustment, and inspection may all be required before the assembly can be delivered.
For OEM manufacturers, controlling these problems at the production stage is more efficient than correcting them after fabrication. Robot Welding can help reduce avoidable variation in repetitive welding operations by combining programmed welding paths, controlled fixtures, stable process parameters, and systematic inspection.
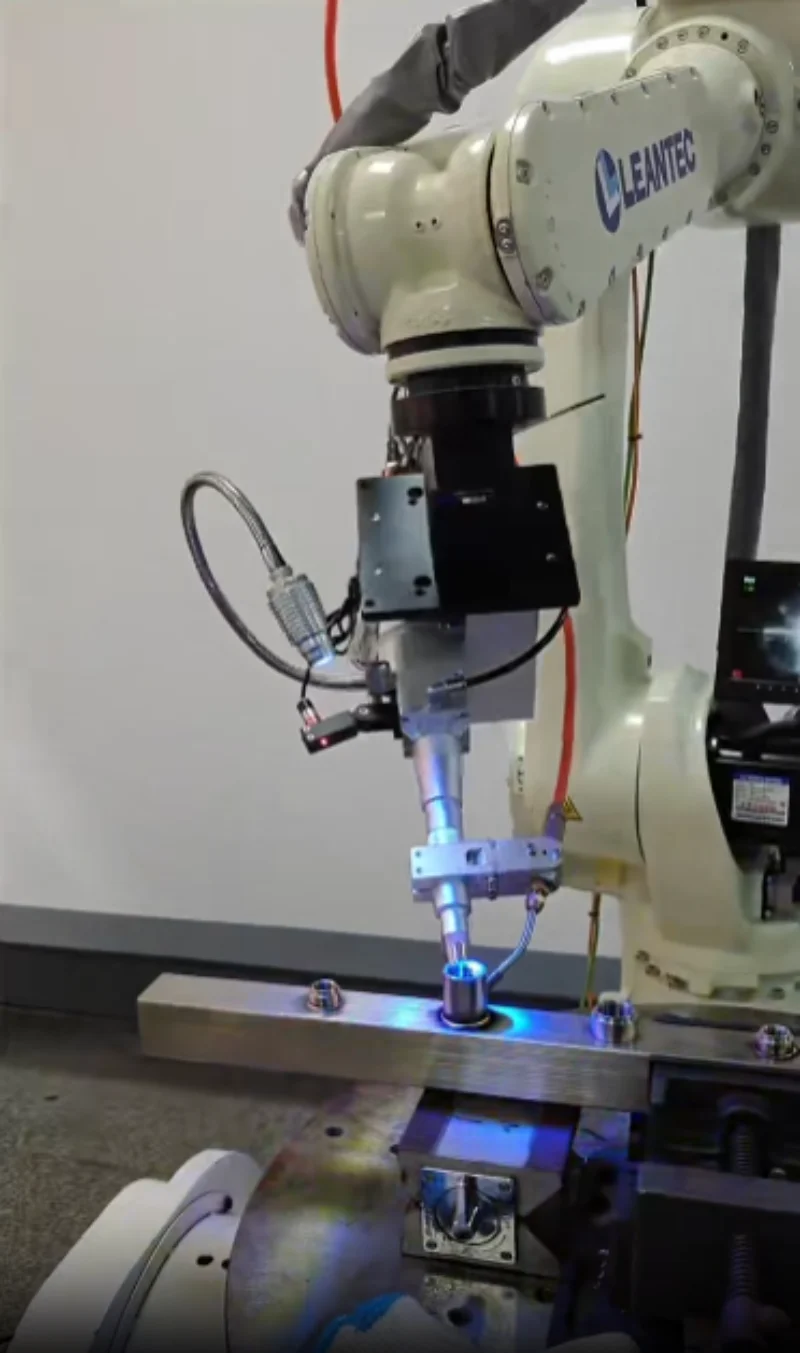
A welded assembly can meet the drawing dimensions before welding and still change shape after the welding process. Heat causes the metal around the joint to expand and contract, creating distortion. If the welding sequence or heat input is not properly controlled, the finished component may require straightening before it can be machined or assembled.
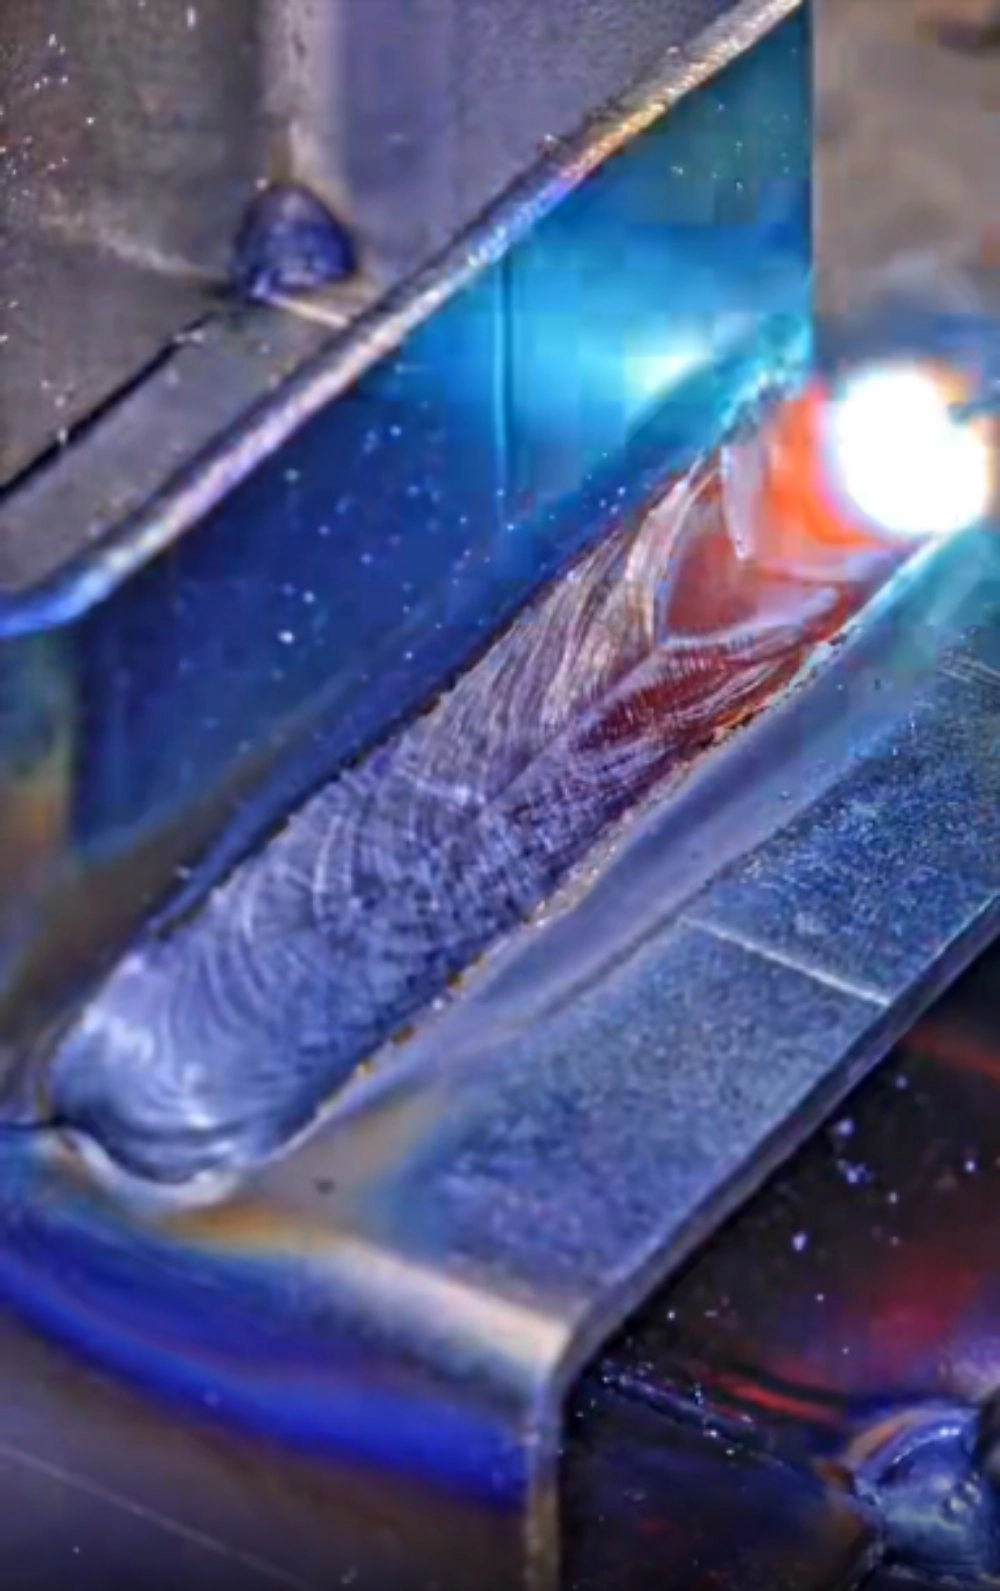
Other common welding problems include porosity, slag inclusion, cracks, incomplete fusion, and inconsistent weld appearance. The impact depends on the application. A minor visual defect on a non-structural component may require cosmetic treatment, while a defect in a pressure-related or load-bearing assembly can affect its functional performance.
For OEM production, repeated defects can also interrupt the production schedule. A batch that requires extensive rework takes additional labor and inspection time, and components may need to return to earlier manufacturing stages.
Reducing these problems therefore requires more than final inspection. The welding process itself needs to be controlled from the beginning.
The main advantage of Robot Welding in repetitive production is process repeatability. Once the welding path, fixture position, and applicable welding parameters have been established, the robotic system can repeat the programmed movement across multiple components.
This is particularly useful for standardized weldments such as compressor frames, equipment bases, construction machinery brackets, welded housings, and other structural assemblies produced in recurring batches.
Manual welding remains appropriate for many parts, especially prototypes, complex geometries, repairs, and low-volume production. However, when a component has a repeatable geometry and a consistent welding sequence, automation can reduce variations caused by differences in manual operation.
Robotic welding does not eliminate the need for engineering control. The quality of the result still depends on joint preparation, fixture accuracy, material condition, welding parameters, and inspection. The purpose of automation is to create a more stable production environment for processes that are suitable for robotic execution.
A robotic welding system follows the programmed path accurately, but the result can still vary if the workpiece is not positioned consistently.
For this reason, fixture design is an important part of the welding process. A properly designed fixture keeps plates, brackets, tubes, and other components in their intended position while the assembly is being welded. It also helps control movement caused by thermal expansion.
For OEM projects, Hehua Machinery Technology (Kunshan) Co., Ltd. can integrate fixture fabrication into its one-stop welding service. Customers can provide drawings, physical samples, or raw materials, and the engineering team can review the structure before production.
Hehua supports 2D CAD as well as STEP, IGS, SolidWorks, and UG 3D files. Reverse engineering is also available for physical samples and legacy weldments. During drawing review, the technical team can identify potential welding deformation and cracking risks and provide DFM optimization suggestions.
This early engineering work can prevent some problems from reaching the welding station in the first place.
Welding deformation is one of the most common reasons a welded assembly may require post-production correction. The degree of distortion depends on factors such as material type, plate thickness, joint configuration, welding sequence, and heat input.
There is no universal welding setting that works for every component. Carbon steel, stainless steel, aluminum alloy, cast iron, ductile iron, and other materials respond differently to heat. The welding process must therefore be selected according to the actual material and application.
Hehua provides MIG/MAG CO2 welding, TIG GTAW argon welding, spot welding, fillet welding, submerged arc welding, brazing, and robotic automatic welding. The appropriate process is selected based on plate thickness, load requirements, material, joint design, and appearance requirements.
After welding, assemblies can undergo straightening and dimensional inspection. For applicable parts, overall dimensional tolerance can reach approximately ±0.1 to ±0.3 mm, while flatness after straightening can reach ≤0.03 mm/100 mm.
These capabilities are particularly useful when a welded component must connect accurately with machined parts or other assemblies.
A robotic welding cell cannot compensate for every upstream material problem. Contamination, incorrect material specifications, poor joint preparation, or dimensional variation in incoming components can all affect welding quality.
Hehua works with carbon steel, galvanized steel, 304/316 stainless steel, aluminum alloy, cast iron, ductile iron, and copper alloy. Material test certificates can be provided, together with material traceability for applicable projects.
Incoming material inspection forms part of the quality control process before welding begins. This provides an additional checkpoint for confirming that the materials entering production are suitable for the specified application.
For projects involving dissimilar metals, the welding method and joint design require additional consideration. The process is evaluated according to the actual material combination and functional requirements rather than applying a standard welding sequence to every project.
Final inspection is important, but waiting until the end of production to discover a problem can result in unnecessary rework. A more practical approach is to introduce inspection at several stages.
Hehua's quality control process includes incoming material inspection, in-process patrol inspection, post-weld straightening checks, and first-article dimensional inspection. Periodic batch inspection can then be used to monitor production consistency.
Welds are checked for defects such as porosity, slag inclusion, and cracks. For critical applications, magnetic particle testing and ultrasonic testing are available. Hydrostatic testing can also be applied to applicable pressure-related assemblies.
Pressure parts receive additional attention. Air and water tightness testing can be performed, with 100% air tightness testing available for pressure components according to project requirements.
This combination of process inspection and final verification helps identify problems before defective assemblies move further into machining, finishing, or customer assembly.
Not every post-weld operation represents a defect. Some processes are a normal part of producing a finished welded assembly.
Straightening, for example, may be required to bring a welded frame back within the specified dimensional range after thermal distortion. Deburring and grinding may also be necessary to remove sharp edges or prepare the surface for subsequent treatment.
Hehua integrates welding with straightening, CNC secondary machining, and surface finishing. Depending on the project, post-weld treatment can include shot blasting, black oxide, electrophoresis, Dacromet, powder coating, galvanization, anodizing, and polishing.
By keeping these processes within an integrated manufacturing workflow, the supplier can coordinate dimensional requirements between welding and downstream operations rather than treating each operation as a separate production stage.
Defect reduction becomes particularly important when an OEM project moves from prototype production to larger batches. A process that works for several samples must also remain stable when production quantities increase.
Hehua supports fast sampling, with typical sample lead times of 3–7 days depending on project requirements. After the first article is completed, dimensions and welding quality can be checked before the process is transferred to recurring production.
For mass production, manual welding stations and automatic robotic welding cells can be used according to the part structure and production requirements. The supporting workshops include cutting, straightening, and polishing, while stamping and CNC machining can also be integrated into the supply chain.
For applicable products, monthly production capacity can reach up to 30,000 sets. This allows the same supplier to support both small-batch development and long-term production programs.
Robotic welding is not automatically the best solution for every welded part. It becomes particularly valuable when the component has a repeatable geometry, stable joint locations, recurring production demand, and a welding sequence that can be reliably programmed.
For low-volume prototypes, highly variable structures, or repair work, manual welding may be more practical. For standardized components produced repeatedly, robotic welding can provide better process repeatability and reduce variation between operators and production cycles.
The decision should therefore be based on the actual component, material, welding requirements, production volume, and expected quality level.
Established in 2005, Hehua Machinery Technology (Kunshan) Co., Ltd. provides key metal parts and components for automotive, rail transit, aerospace, wind power, nuclear power, industrial machinery, semiconductor equipment, new energy equipment, and other high-end equipment manufacturing applications.
Hehua operates a manufacturing plant of more than 17,800 square meters with over 160 employees. The company has obtained ISO 9001 quality management system certification, IATF 16949 automotive quality system certification, and EN 15085 rail vehicle and parts welding system certification. Its welders have also obtained EN ISO 9606-1 qualification certification.
The company's project technical team supports the process from design and development through manufacturing. Production and project information is managed through an ERP system covering sales, projects, production, inventory, procurement, and other operational functions.
For overseas OEM customers, Hehua also provides production-to-export support, technical communication, inspection documentation, and remote technical assistance.
The most effective way to reduce welding defects is not simply to repair defective parts faster. It is to reduce the conditions that create defects in the first place.
Fixture design, material verification, welding process selection, robotic repeatability, DFM review, deformation control, in-process inspection, and post-weld testing all contribute to a more stable manufacturing process.
For suitable repetitive production, Robot Welding can reduce process variation while supporting consistent welding operations across larger batches. When combined with straightening, CNC machining, inspection, surface treatment, and technical support, it becomes part of a complete approach to controlling quality and minimizing unnecessary production rework.
For OEM manufacturers that need repeatable welded assemblies with documented quality control, Robot Welding provides a practical option for moving from prototype development to stable production while keeping welding quality, dimensional accuracy, and rework under control.

 AddressNo. 66 Xingpu Road, Lujia Town,Kunshan City, Factory Buildings 3 and 4
 en
 English
 繁体中文
 Italian
 Spanish
 Japanese
 Portuguese
 Korean
 Russian
 French
 German
 Estonian
 Arabic
 Indonesian



 Message